
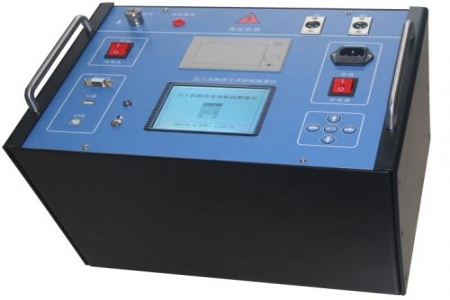
During steam turbine maintenance, it is common for field operation and maintenance personnel to encounter situations where the bolt electric heating rod does not heat up after being inserted into the center hole, or the bolt elongation fails to meet requirements after a period of heating. Such problems are often related to the parameter selection of the heating rod itself, the fit clearance, and the matching of the control cabinet. The following provides a one-by-one explanation of several key issues regarding bolt electric heating rods from the perspective of on-site comparative analysis.
The hard tube type heating rod uses a rigid stainless steel sleeve with relatively high dimensional accuracy, and its straightness can be controlled to about φ0.3mm within 1 meter. If the bolt center hole is straight with no obvious bending, the hard tube type can be inserted smoothly and the heat transfer path is stable. The flexible tube type can be bent to a moderate degree, making it suitable for long bolts or occasions where the hole channel has slight deformation, but the surface power density distribution will change somewhat after bending, and local temperature needs attention. The semi-flexible type falls between the two and is suitable for medium-length bolts. During on-site judgment, a plug gauge or borescope can first be used to confirm the straightness of the center hole, and then the structural form can be determined.
Bolt electric heating rods are equipped with aviation plugs as standard, mainly to solve the problems of quick plugging and unplugging and preventing incorrect connection. During steam turbine maintenance, multiple heating rods need to be connected to the control cabinet at the same time, and ordinary terminal wiring can easily confuse phase sequence and circuit numbers. Aviation plugs are positioned by keyways, so they cannot be inserted in the wrong direction, reducing misoperation. In addition, the contact resistance of aviation plugs is relatively stable, and good electrical conductivity can still be maintained after repeated disassembly and assembly. Ordinary terminals require checking wire numbers one by one, resulting in lower disassembly and assembly efficiency, and loose screws after long-term use may also cause poor contact.
Surface power density is usually controlled at 8–11W/cm². If the value is too low, the heating speed is slow, and the typical working condition of rising to 450°C within 30 minutes may not be met; if the value is too high, the local surface temperature of the heating rod can easily exceed the allowable range of the bolt material, causing changes in the bolt metallographic structure. During on-site comparison, if the heating time is found to be significantly prolonged while the control cabinet output voltage is normal, check whether there is scale accumulation on the surface of the heating rod or whether the magnesium oxide powder has absorbed moisture. Moisture absorption will reduce insulation resistance and also affect thermal conductivity.
The total clearance between the heater outer diameter and the bolt center hole is recommended to be controlled at 0.8–1.3mm. If the clearance is too small, the heating rod is difficult to insert or may even become stuck, and the heating rod sleeve is easily damaged during removal; if the clearance is too large, the thermal resistance of the air layer increases, heat transfer efficiency decreases, and bolt elongation is insufficient. When insertion difficulty is encountered on site, do not force it in by hammering; instead, measure the center hole diameter and the heating rod outer diameter to confirm whether they are within the fit range. After long-term use, scale or oil contamination may accumulate on the inner wall of the center hole, which will also affect the clearance. It is recommended to clean the hole channel during maintenance.
The cold-state insulation resistance is required to be no less than 50MΩ (DC500V), and no less than 100MΩ under working conditions. During on-site testing, if the insulation resistance is lower than the standard, the common cause is failure of the cold-end seal, allowing moisture to enter the magnesium oxide powder layer. Magnesium oxide powder must be used after drying, and moisture should also be avoided during storage and installation. The treatment method is to dry the heating rod at low temperature in an oven and use it after the insulation resistance recovers. If it still does not meet the standard after drying, there may be a short circuit between the heating wire and the sleeve, and the heating rod needs to be replaced. The shell must be reliably grounded, and the withstand voltage strength should be tested according to AC2000V/1min without breakdown.
For flammable and explosive environments such as petrochemical and natural gas facilities, an ExdⅡBT4 flameproof structure should be selected. Using ordinary heating rods in explosion-proof areas poses safety risks, and the control cabinet should also have the corresponding explosion-proof rating. During on-site replacement, the explosion-proof marking on the heating rod nameplate must be checked, and an ordinary type cannot be used to replace an explosion-proof type. The wiring cavity and plug parts of explosion-proof heating rods both have flameproof structures, and they should be operated in accordance with explosion-proof requirements during disassembly and assembly to avoid damaging the flameproof surfaces.

